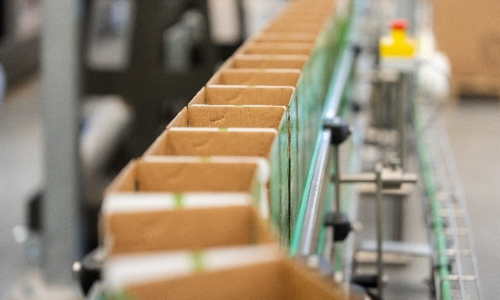
An integrated solution combining automation and packaging made it possible to increase output from 1,500 to 1,900 boxes per hour, reduce labor requirements, and increase storage capacity.
As retailers and manufacturers face growing pressure to improve productivity and ensure consistent product availability, DS Smith, a global provider of sustainable packaging, has collaborated with Delhaize, an international retail and wholesale holding company, to increase the output of a wine packaging line by 27%. At Delhaize’s Belgian winery, the two companies redesigned both the packaging and the machinery used to process it, boosting productivity by an additional 400 boxes per hour.
The project focused specifically on Ahold Delhaize’s range of Bag-in-Box (BiB) wines. The Zellik facility produces wines for Delhaize in Belgium and Albert Heijn in the Netherlands, making production efficiency and reliability essential to ensuring a smooth supply chain across multiple markets. Despite a highly competitive market, the Delhaize brand has demonstrated resilience and is recording sales growth in Bag-in-Box wines. As this packaging format plays an increasingly important role in its portfolio, Delhaize sought to expand capacity and drive further efficiency across its entire production process.
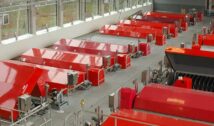
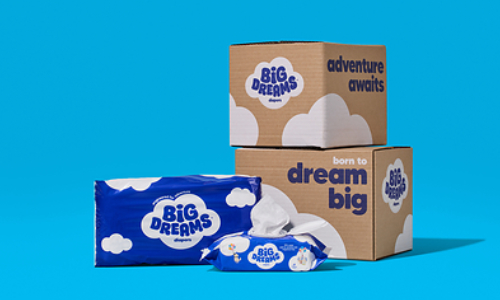
To meet this challenge, Delhaize opted for an integrated approach. Rather than sourcing corrugated packaging and end-of-line packaging machinery separately, DS Smith and Delhaize partnered to design and build a bespoke mandrel case erector tailored to the Delhaize Bag-in-Box format and its production requirements. This machine ensures optimal efficiency and productivity throughout the entire packaging process—erecting, filling, sealing, and palletizing—by virtually eliminating line stoppages and improving case squareness.
Thanks to this new approach, packaging performance has improved and production speeds have increased from 1,500 to 1,900 boxes per hour, representing a 27% rise. The production line has become more reliable and requires fewer operators, allowing staff to be reallocated to strengthen quality control. Storage capacity has also improved, rising from 5,000 to 6,000 boxes in each warehouse.
The Bag-in-Box packs feature high-quality offset printing for strong visual impact on the shelf and a high-end product perception among consumers. The brand is also strengthened, with a clear focus on premium positioning.
“What sets DS Smith apart is its ability to design and optimize packaging and machinery as a single, unified solution,” said Hervé Louis, Sales Marketing & Innovation Director at Delhaize Belgium. “The interaction between these two elements is decisive, and by combining them from the outset, we were able to increase throughput, reduce downtime, and make better use of our existing capacity. I am impressed by DS Smith’s level of service.”
Kim Radelet, Sales Marketing & Innovation Director at DS Smith Central EMEA, added: “This project shows that the greatest opportunities for improvement often lie beyond the packaging itself. By looking at the entire system—from packaging design and materials to machinery performance, warehousing, and operational efficiency—we enabled Delhaize to unlock 27% additional capacity from its existing operation. That is where true value is created: not by optimizing isolated elements, but by improving performance across the entire value chain.”
Delhaize store banners include Delhaize, Maxi, Albert Heijn, Albert, Food Lion, Gall & Gall, Mega Image, Alpha-Beta, Hannaford, Stop & Shop, and The GIANT Company, offering a wide range of traditional supermarkets and online grocery shopping.
DS Smith has established a purpose-led sustainability strategy and is committed to leading the industry-wide transition to a circular economy, while providing sustainable circular solutions to its customers worldwide.
Photo/DS Smith
RELATED NEWS